Explore our flagship heavy-duty industrial storage racks, multi-tier mezzanine floor platforms, and high-cube structural equipment engineered for maximum structural density, payload optimization, and seamless intermodal compatibility across global supply networks.
In an era characterized by dynamic global trade shifts, supply chain recalibration, and intense operational pressure, international enterprises require robust, resilient, and highly scalable material handling solutions. As a preeminent global logistics hardware manufacturing hub, China produces over 85% of the world’s intermodal shipping containers, specialized freight storage units, and structural warehouse racking infrastructure. Navigating the selection of a China Top Shipping Containers Supplier & Exporter demands rigorous evaluation of engineering compliance, alloy metallurgy, load capacity ratings, and lifecycle cost optimization.
Modern intermodal freight logistics and warehouse distribution centers are no longer isolated silos; they form a continuous dynamic ecosystem. Intermodal shipping containers serve as the macro-vessel for oceanic and overland transit, while modular steel mezzanine platforms and heavy-duty pallet racking systems act as the internal micro-density engine within fulfillment hubs. The convergence of structural steel engineering across intermodal containers and heavy-duty storage racks has enabled global procurement officers to streamline vendor networks, leveraging unified manufacturing standards to minimize logistics friction and structural downtime.
Mitigating geopolitical disruption through high-volume, standard-compliant steel manufacturing. Integrated production ensures consistent quality from intermodal containers to high-bay racking systems.
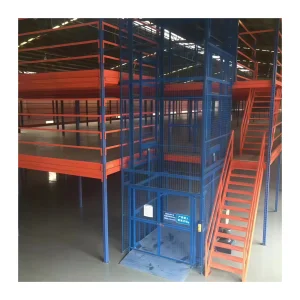
Vertical volumetric optimization utilizing multi-layer structural mezzanine platforms and high-cube ISO containers, doubling usable footprint without expanding physical real estate acquisition costs.
Strict adherence to international standards (ISO 9001, FEM 10.2.02, ANSI MH16.1, EN 15512), enforced by certified quality control engineers and advanced non-destructive weld testing.
The global material handling and intermodal freight equipment market is undergoing a structural transformation. Key growth drivers include the exponential rise of global cross-border e-commerce, automated warehouse integration (ASRS), and green manufacturing initiatives designed to reduce lifecycle carbon footprints.
Modern intermodal shipping containers and warehouse pallet racks are evolving toward fully modular, boltless, and field-configurable structural architectures. High-yield Q235B and Q355B cold-rolled steel profiles allow rapid field installation and dynamic re-configurability as inventory volumes shift.
Transitioning from conventional solvent paints to high-durability electrostatic thermosetting powder coatings and hot-dip galvanization. Standardized salt-spray resistance exceeding 1,000 hours guarantees longevity in harsh maritime and high-humidity cold-chain environments.
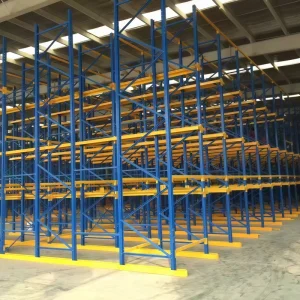
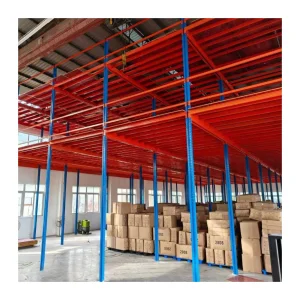
With urban industrial real estate costs soaring globally, enterprises are pivoting from horizontal expansion to multi-tier steel mezzanine floors and high-density deep pallet racking, tripling effective storage cubic meter metrics.
Through intent mining of global supply chain directors, procurement managers, and logistics engineering consultants across North America, Europe, Australia, and the Middle East, we have identified five primary evaluation criteria governing large-scale container and racking contracts:
Verification of ultimate tensile strength, yield points, dynamic deflection limits under full payload, and seismic zone safety compliance ratios (minimum 1.5 safety factor).
Balancing initial CAPEX against longevity, maintenance downtime, modular repair costs, and container freight shipping density optimization (knock-down packaging design).
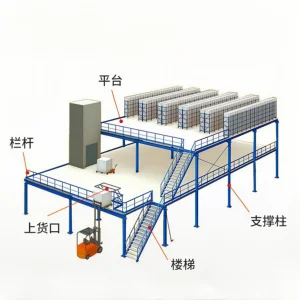
Customization flexibilities including structural pitch adjustments, custom colors (RAL system), perforated beam profiles, and integrated mezzanine staircases/catwalks.
Verified ISO9001 quality systems, environmental management compliance, traceable steel mill certifications, and transparent third-party loading test protocols.
Guangdong Guanlongxing Storage Equipment Co., Ltd. is a professional manufacturer specializing in warehouse storage racks, industrial shelving systems, pallet racking, mezzanine platforms, and customized storage solutions. Since its establishment in 2017, the company has been committed to delivering reliable, cost-effective, and high-performance storage equipment for warehouses, distribution centers, logistics companies, factories, supermarkets, and retail facilities worldwide.
Operating from a modern manufacturing facility covering 28,600 m², Guanlong Rack integrates product design, engineering, manufacturing, quality control, and international sales under one roof. Our experienced production team and advanced manufacturing equipment enable us to deliver efficient production, consistent quality, and flexible customization for projects of all sizes.
With over 9 years of industry experience and 6 years of export experience, we have built strong partnerships with customers across Europe, North America, Southeast Asia, Australia, and the Middle East. Our annual export revenue exceeds US$18 million, supported by an efficient supply chain of more than 980 trusted partners.
Quality is at the core of everything we do. Every product undergoes rigorous inspections throughout the manufacturing process, including load capacity testing, dimensional inspection, welding inspection, and powder coating adhesion testing. Our dedicated quality control team of 46 inspectors ensures every shipment meets international standards before delivery.
Innovation drives our continuous growth. Our R&D department consists of 62 experienced engineers focused on improving structural design, production efficiency, and warehouse storage solutions. Last year alone, we introduced 136 new products to meet evolving market demands and customer requirements.
We provide comprehensive OEM and ODM manufacturing services, supporting customized dimensions, load capacities, colors, materials, and warehouse layouts based on each customer's project needs. Our flexible production capabilities make us a reliable partner for distributors, wholesalers, warehouse solution providers, contractors, and engineering companies.
At Guanlong Rack, our mission is to help customers maximize warehouse efficiency with durable, safe, and intelligent storage systems. Through advanced manufacturing, strict quality management, and responsive customer service, we continue to provide dependable storage solutions that create long-term value for businesses around the world.
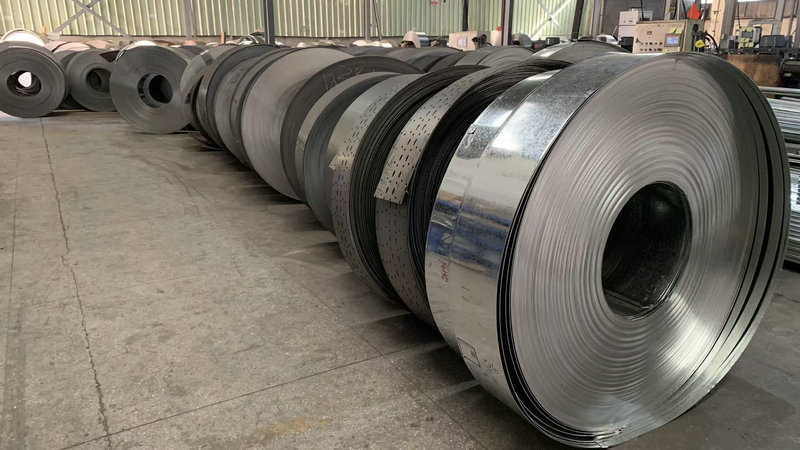
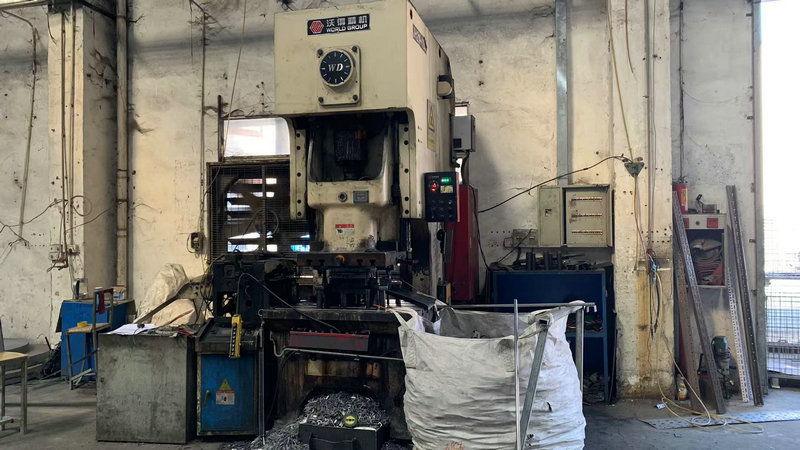
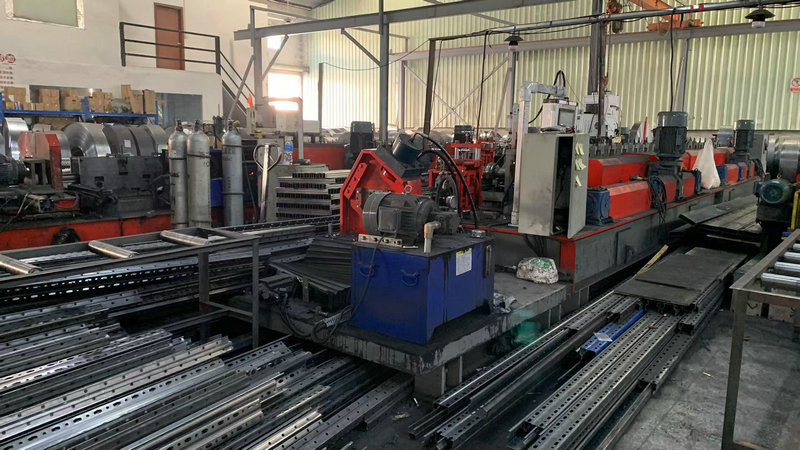
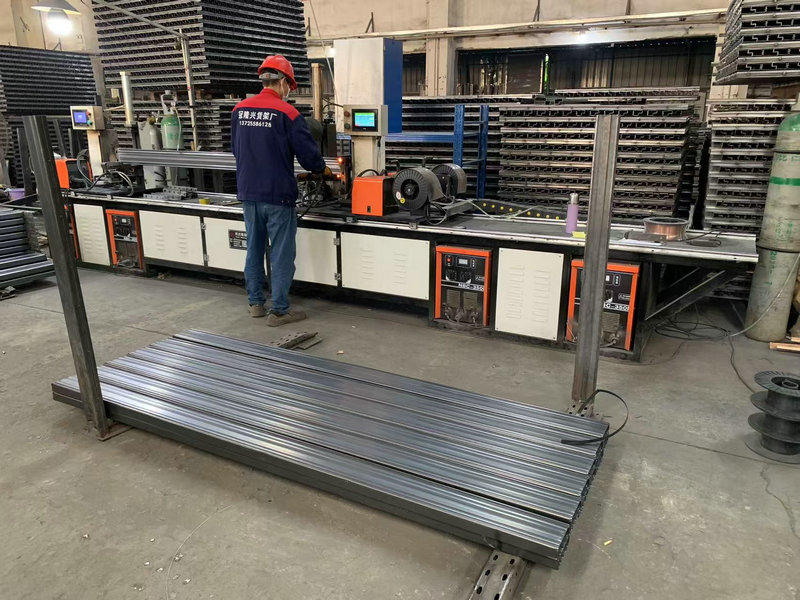
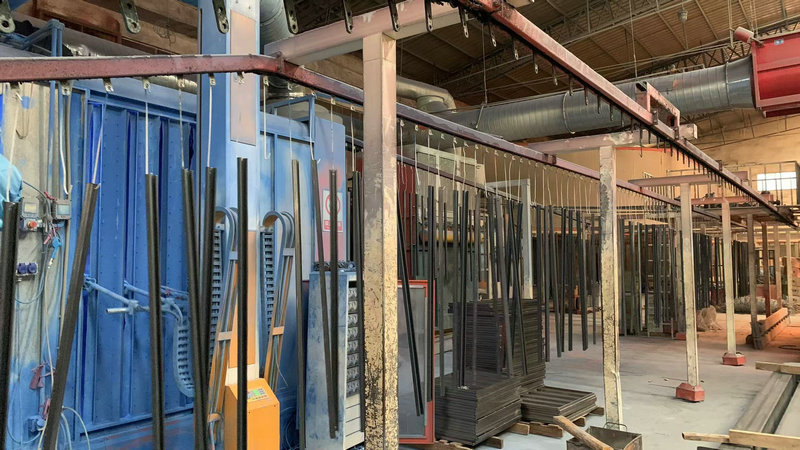
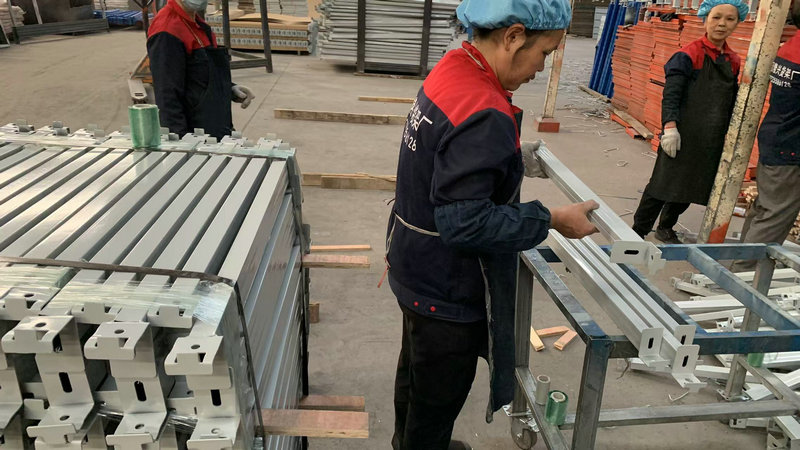
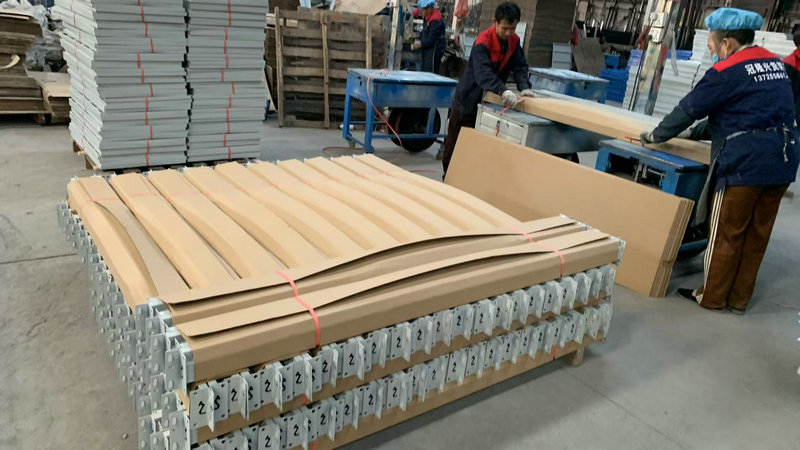
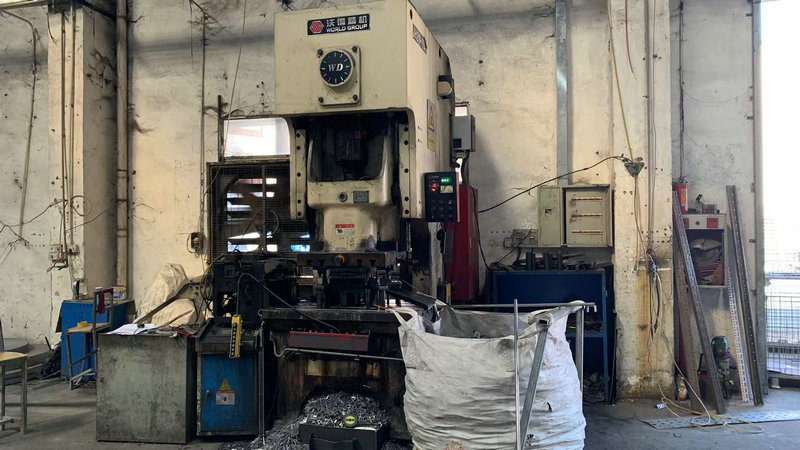
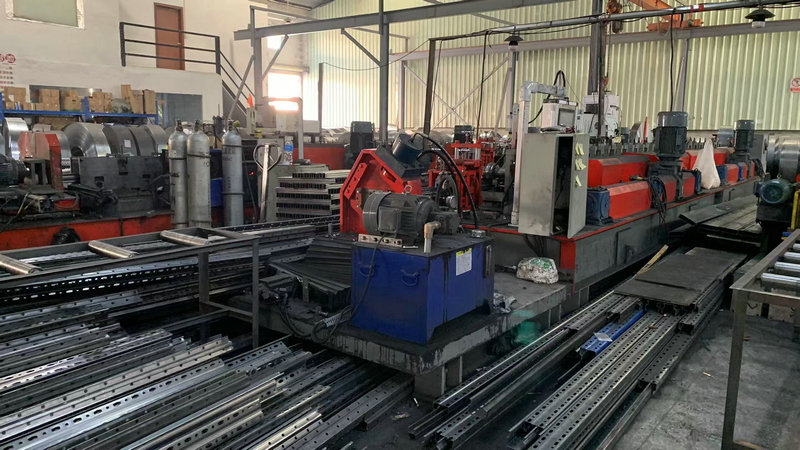
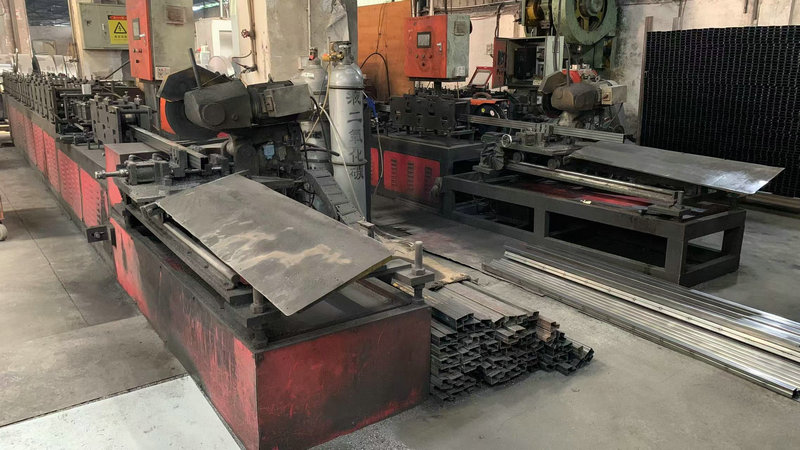
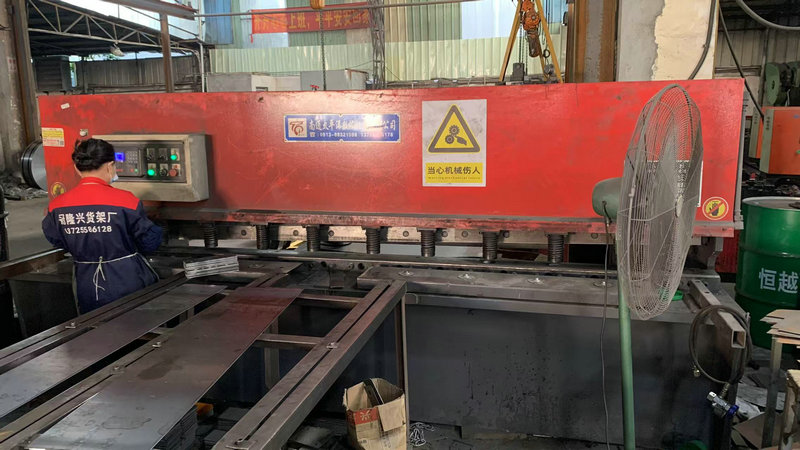
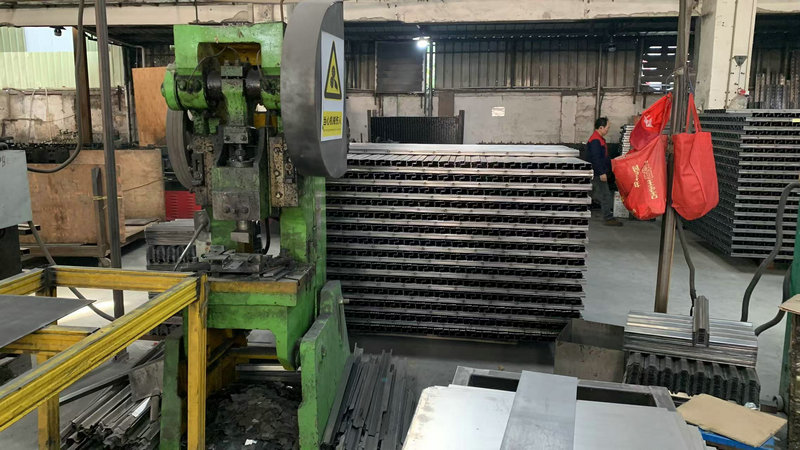
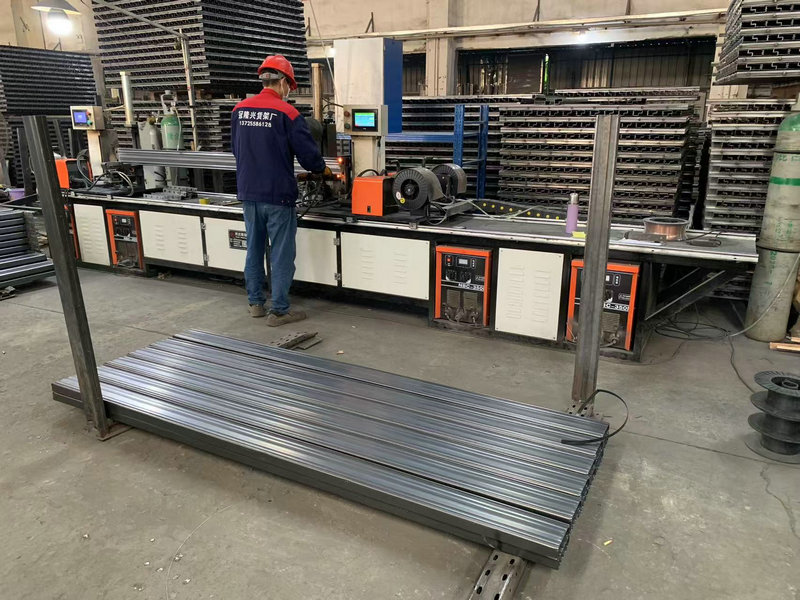
Our state-of-the-art Pearl River Delta factory houses fully automated continuous cold-roll forming production lines, robotic multi-point welding cells, and eco-friendly automatic electrostatic powder coating channels. Explore our end-to-end manufacturing flow below:
Guangdong Guanlongxing’s specialized storage racking and intermodal freight equipment are deployed across diverse high-demand global operational landscapes:
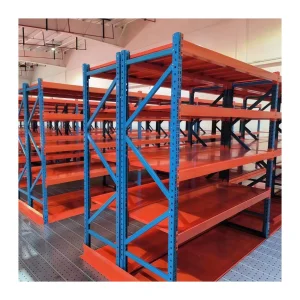
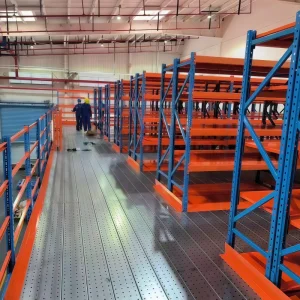
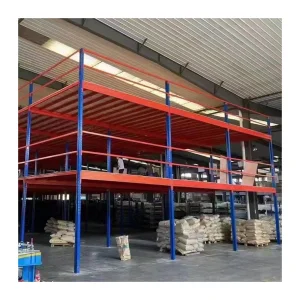
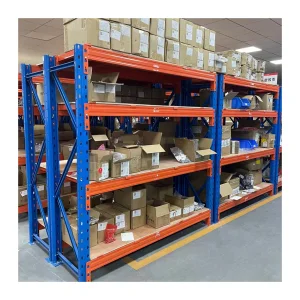
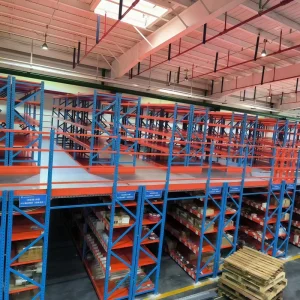
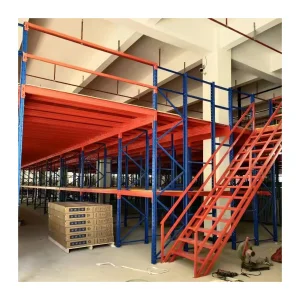
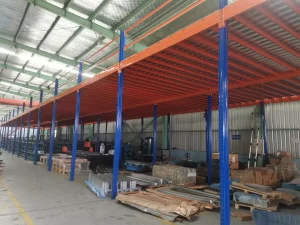
Deployment: Multi-layer mezzanine platform systems with high-density long-span shelving.
Impact: Achieves a 300% increase in SKU pick-face density in high-velocity fulfillment hubs across Germany, Netherlands, and USA.
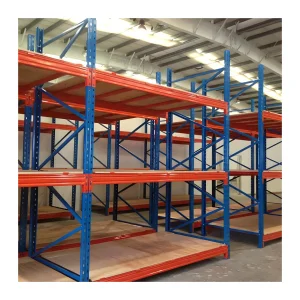
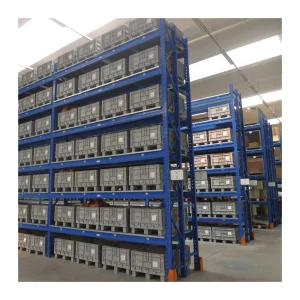
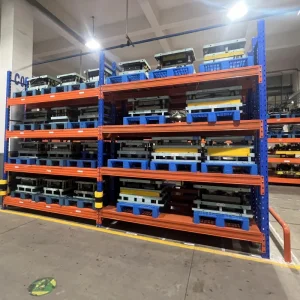
Deployment: Heavy-duty selective pallet racking engineered for up to 4,000 kg load capacity per tier.
Impact: Serves automotive assembly plants and heavy machinery fabricators across Australia and Saudi Arabia.
Deployment: Hot-dip galvanized metal racking systems and specialized shipping container storage frames.
Impact: Resists sub-zero corrosion and thermal shock down to -30°C in seafood and pharmaceutical logistics in Norway and Japan.
To provide complete technical transparency for enterprise structural engineers, the table below outlines the material properties, manufacturing tolerances, and compliance parameters of Guanlongxing industrial storage systems compared to standard market alternatives:
| Engineering Parameter | Guanlongxing High-Spec Standard | Standard Industry Average | Operational Impact |
|---|---|---|---|
| Primary Steel Grade | Certified Q235B / Q355B Cold-Rolled Steel | Recycled Commercial Grade Steel | +25% Higher Yield Strength & Fatigue Resistance |
| Surface Protection | Epoxy-Polyester Electrostatic Powder (60-80μm) | Single-Layer Solvent Painting (30-40μm) | Superior Scratch Resistance & 1000h Salt-Spray Rating |
| Beam Hole Pitch Adjustability | Precision 50mm / 75mm Pitch Punching | 75mm or Fixed Pitch | Maximizes Vertical Cubic Utility for Varied Pallet Heights |
| Quality Control Testing | 100% Load Cell Deflection & Weld Ultrasonic Testing | Random Batch Inspection | Zero Defect Safety Rating Under Maximum Load |
| Structural Design Compliance | FEM 10.2.02, EN 15512, ANSI MH16.1 Certified | Basic Regional Standards | Seamless Global Building Code Approval |
Addressing critical technical, regulatory, and purchasing inquiries from international sourcing buyers:
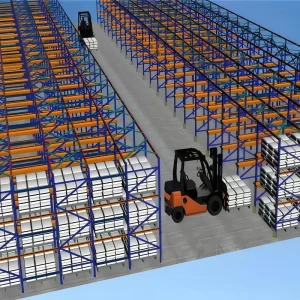
Discover our high-bay pallet racking systems, heavy-duty mezzanine platforms, and multi-layer structural shelving engineered for maximum spatial efficiency and demanding industrial operations.
 Guanlong Rack